Core Services / INP Centre
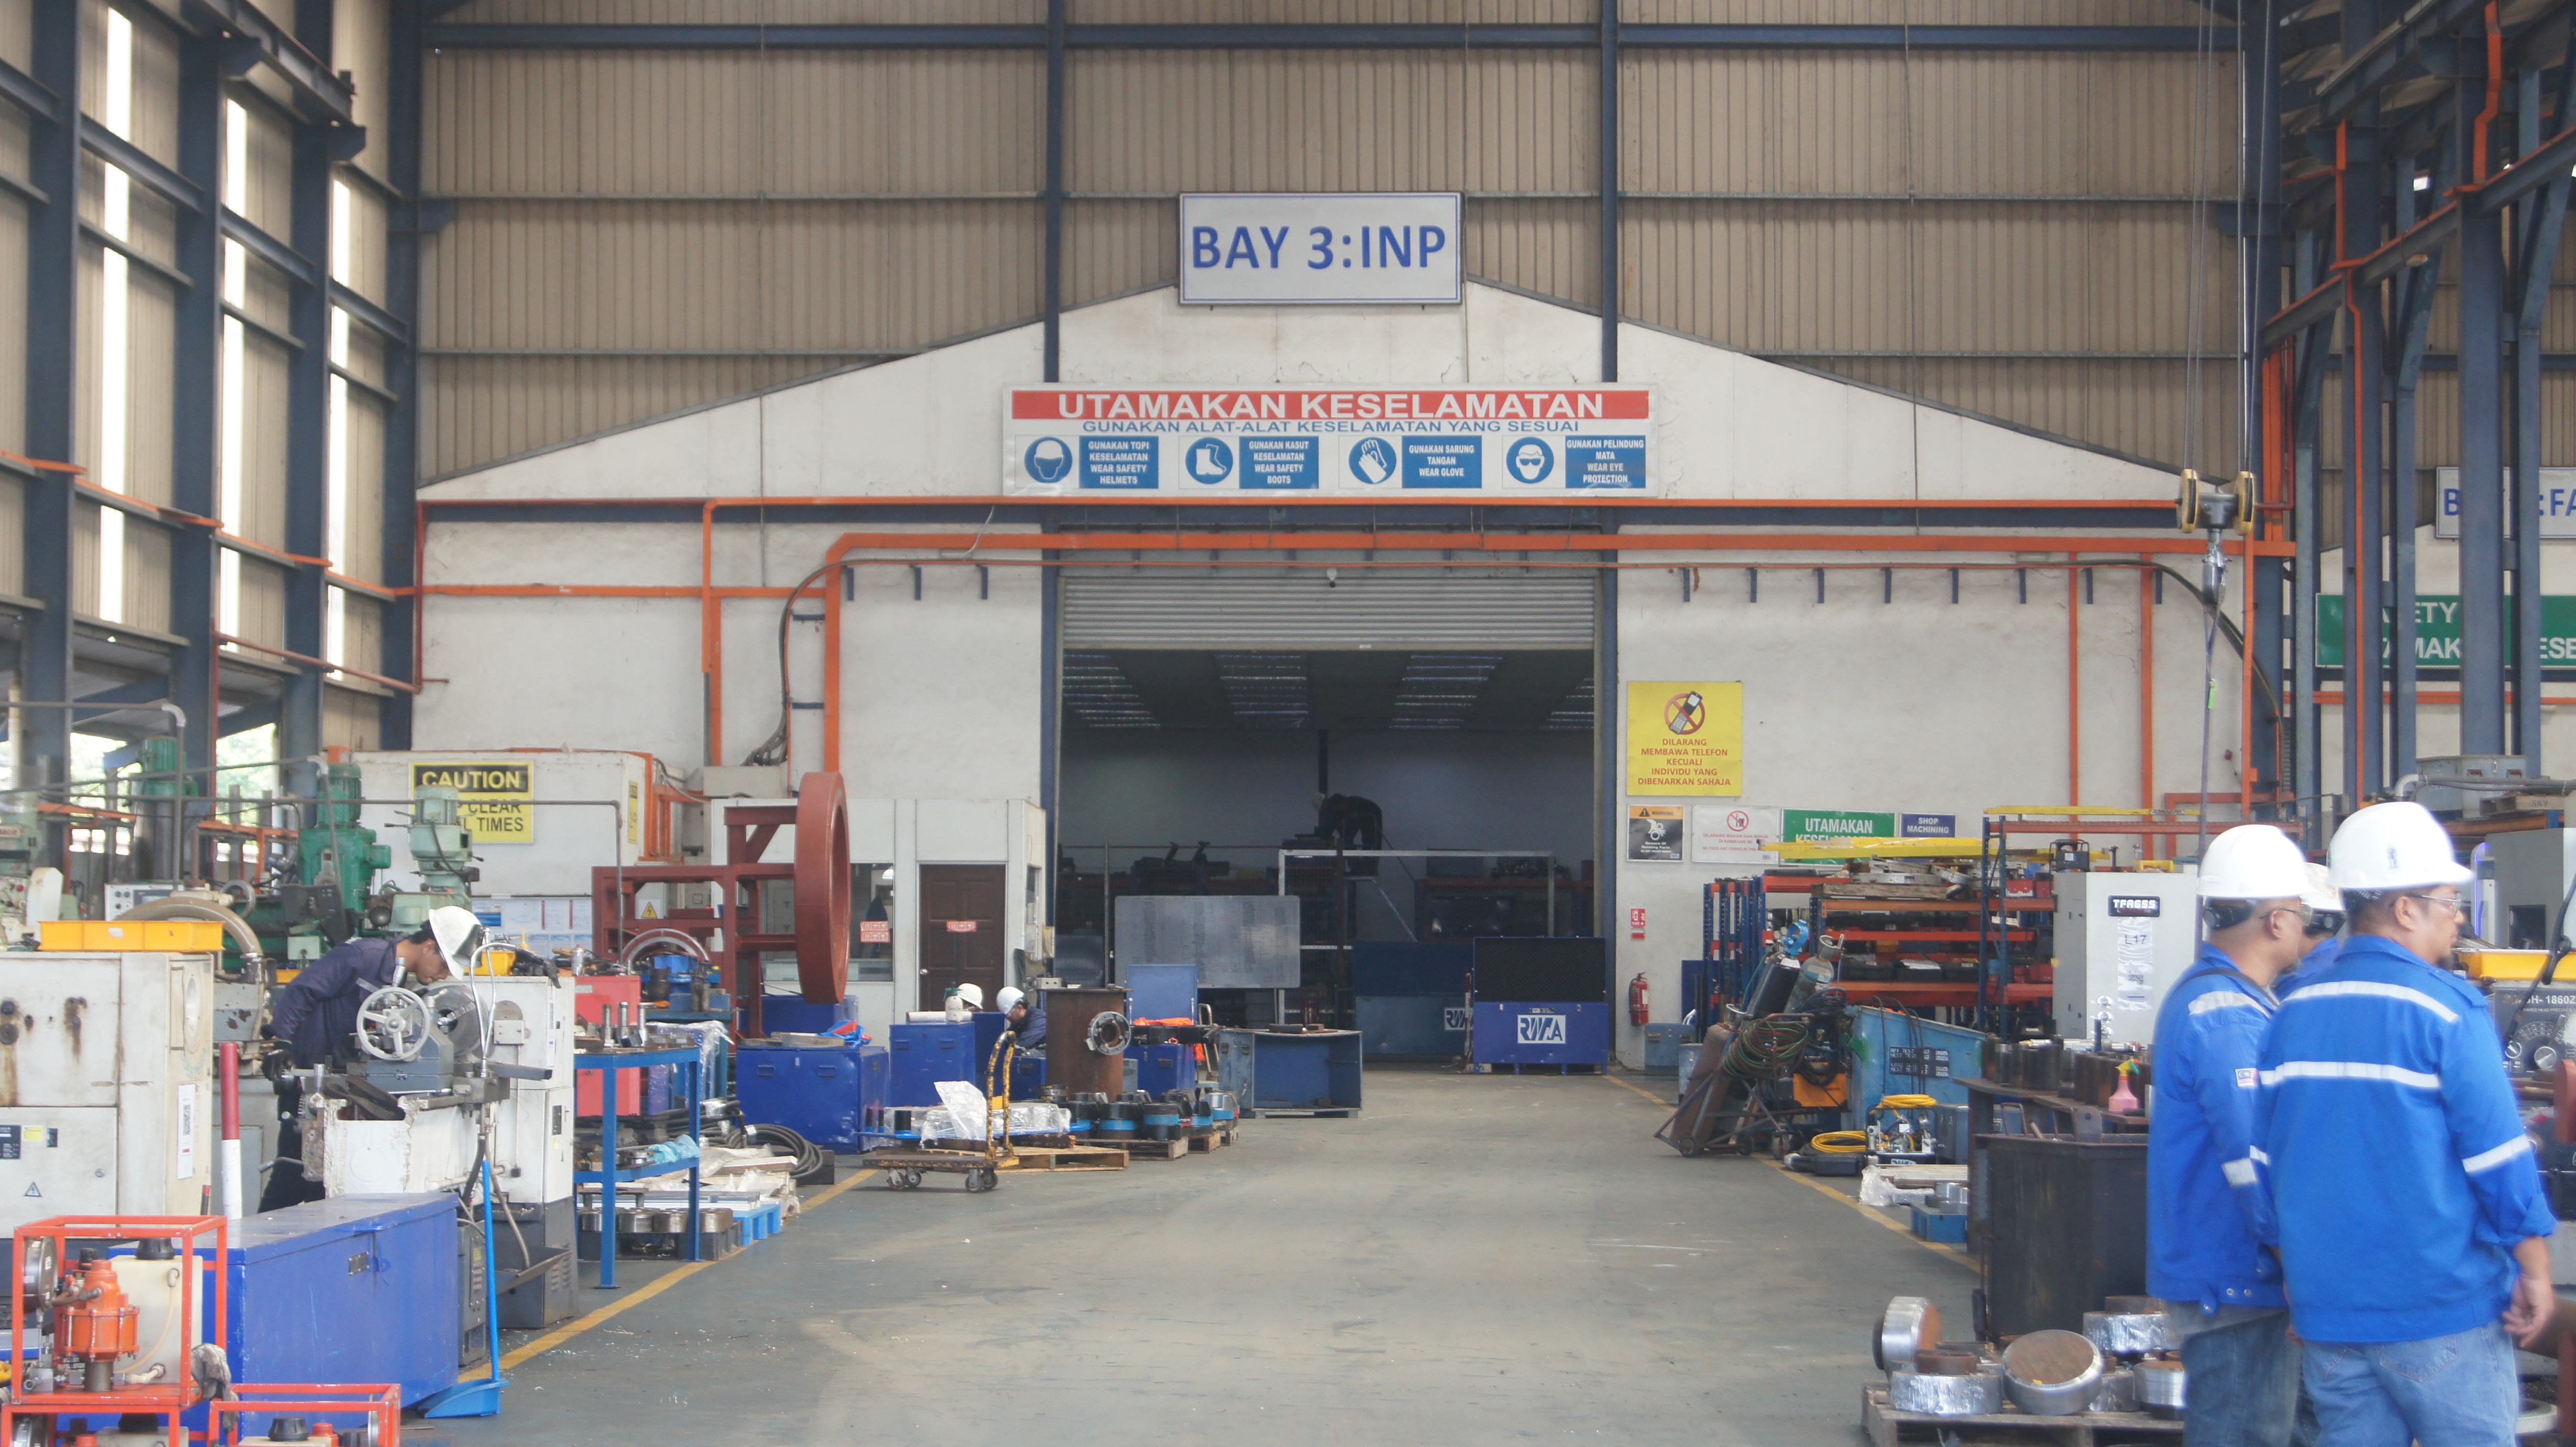
Our state-of-the-art facility — the backbone for precision engineering, R&D, and custom manufacturing solutions.
Our Direction
Three guiding principles that drive everything the INP centre does.
To become a "One Stop Solutions Provider" company for Oil & Gas, Maintenance, Machining, and R&D industries.
To provide the best technical and operational know-how, adopting the highest stringent HSE practices in delivering quality products and services within agreed time frames.
To be at the forefront of innovative and customised designing, new product development, and quality machining for internal and external customers.
Objectives & Functions
Custom engineering design and CAD/CAM solutions.
Research and development for innovative product development.
State-of-the-art CNC machining capabilities.
Production and support services for internal and external clients.
Our Capabilities
Every capability in our centre is a machining discipline. Sawing, turning, milling, grinding, drilling — each section runs dedicated equipment operated by experienced machinists, handling the full range of materials and tolerances demanded by oil and gas service.
Every job starts here. Our sawing section cuts raw bars, plates, and billets down to working sizes, ready for the machines downstream.
Bandsaws handle the bulk of our cutting across ferrous and non-ferrous materials, in capacities from 9-inch up to 16-inch NC-controlled units. For hardened materials and intricate profiles, wire cutting delivers precision that conventional blades cannot match.
The workpiece spins, the tool cuts. Turning is how we produce shafts, sleeves, flanges, valve bodies, and threaded connections.
Our conventional lathes cover everyday work with the flexibility that one-off jobs demand. For large-diameter and heavy components, our single and double column vertical lathes take on workpieces that would be impractical anywhere else — a critical capability for oversized valve bodies, flanges, and pump casings common in oil and gas service.
The tool spins, the workpiece moves. Milling produces flat surfaces, slots, pockets, and complex contours across plates and blocks.
Our vertical milling machines handle general machining, fixture building, and component finishing. Backed by CNC milling centres, we move seamlessly from one-off manual work to repeatable, programmed production.
Where tolerance and finish matter most. Grinding and lapping remove the last microns of material to deliver surfaces that turning and milling alone cannot achieve.
Cylindrical and surface grinders bring shafts and flat faces to specification. Lapping takes it further, producing mirror finishes critical for valve seats and sealing surfaces where even microscopic imperfections cause leakage. Our ball grinding and seat ring lapping capability is purpose-built for the valve refurbishment work at the heart of our service offering.
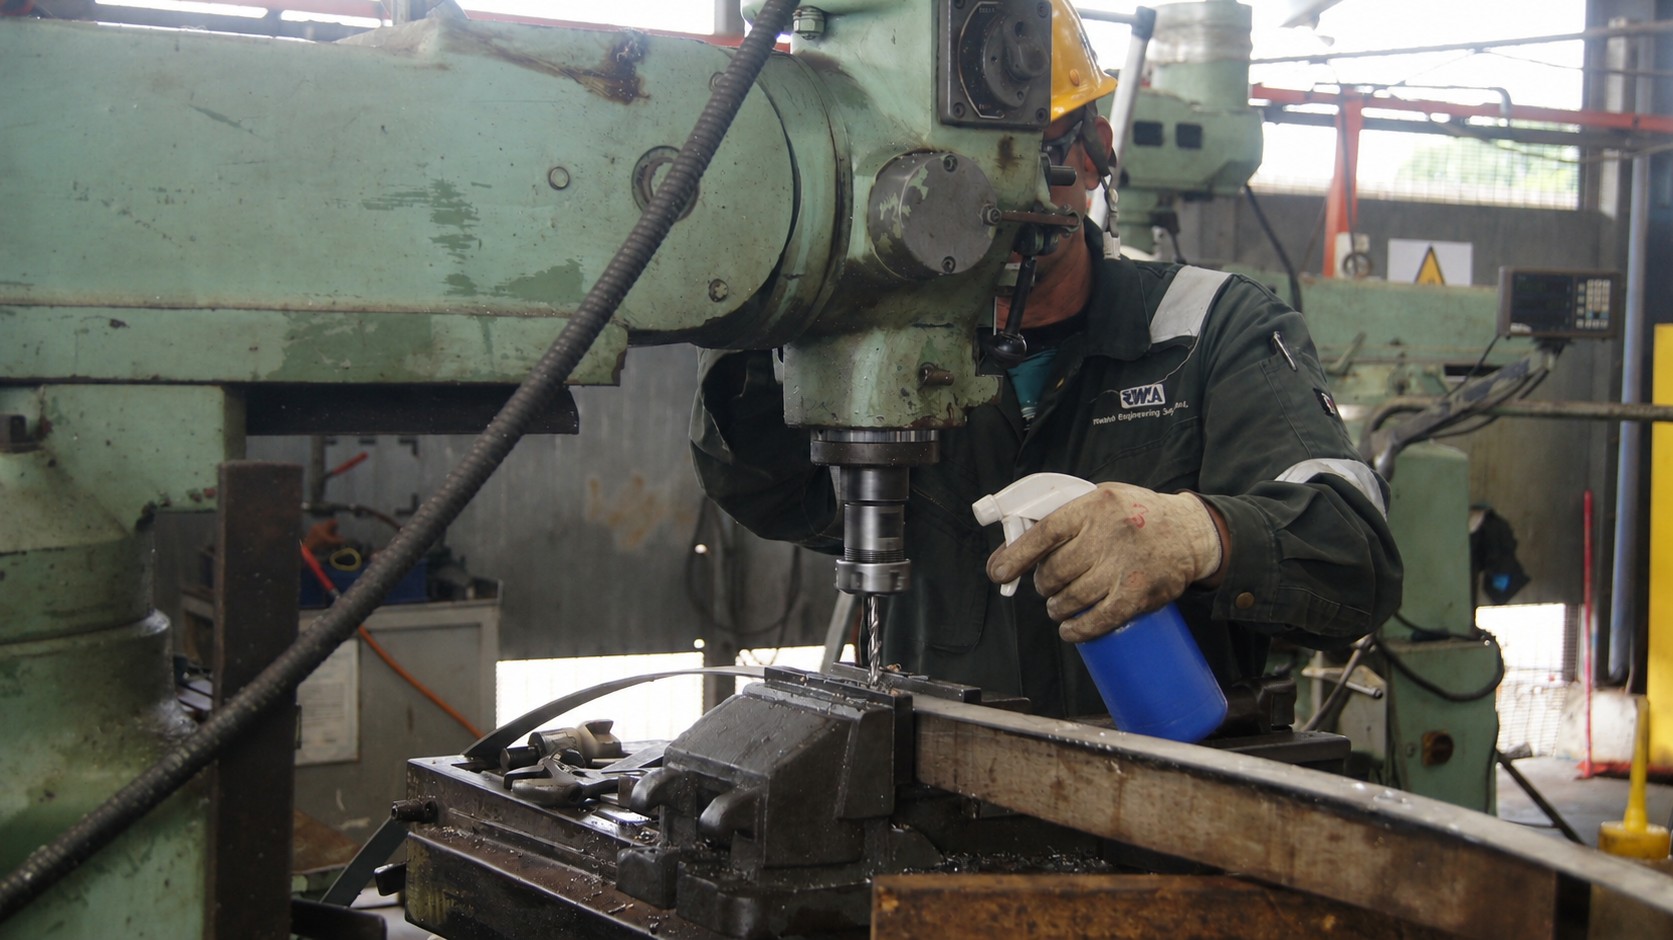
For the jobs that need a different approach. Radial arm drills reach into large and awkward workpieces where standard drill presses cannot. Slotting machines cut internal keyways, splines, and square features that no mill can produce.
Machined, assembled, but not yet certified. Every valve we service is proven on our test benches before it leaves the centre.
Hydraulic test benches verify body integrity and seat tightness across the full pressure range. Dedicated safety valve test benches certify the set pressure at which relief valves open — a non-negotiable requirement in oil and gas operations. Our bench capacity spans ½” to 12” valves, covering the vast majority of inline and safety valves in service across the industry.
Precision at Scale
CNC (Computer Numerical Control) is the backbone of our production capacity. Where conventional machines depend on the operator's hands, CNC machines work from digital programs, moving the cutting tool along multiple axes simultaneously to micron-level accuracy.
The hundredth part matches the first. Essential for batch production of valve internals, sleeves, and mating components.
Contoured surfaces, precise tapers, and intricate profiles — routine on a CNC, impossible on a conventional machine.
Once proven, a CNC program runs largely unattended. Our machinists focus on setup and the work that genuinely needs human judgement, while the machine delivers consistent output.
Our CNC capability spans turning, 3-axis vertical milling, and NC-controlled sawing, giving us the range to handle prototypes, refurbishment work, and repeat production runs from the same shop floor.
Under CNC
EDM removes material through controlled electrical sparks rather than cutting — enabling shapes and tolerances that conventional tooling cannot reach, particularly in hardened metals where physical cutting tools would fail or deflect.
A thin wire electrode traverses the workpiece under CNC control, cutting complex 2D profiles through any electrically conductive material — regardless of hardness. Used for precision dies, punches, intricate slots, and profiles that are impractical to mill or grind.
A rotating tubular electrode burns deep, precise holes at high speed — including in hardened tool steels and difficult alloys. Ideal for small-diameter deep holes, cooling channels, and start holes for wirecut operations where conventional drills would deflect or break.
Because material is removed by spark erosion rather than mechanical cutting, EDM works on any conductive metal regardless of hardness — after heat treatment, after hardening, after all other machining is complete.